How to Handle Multi-Product Orders in a Print-on-Demand Operation
TLDR: Handle multi product print on demand orders by treating the customer order as the control unit and each product line as a linked work packet. Batch compatible lines for efficient production, but retain the parent order ID through printing, finishing, quality control, consolidation, packing, and shipping. Release the shipment only when every required line passes a positive reconciliation—or when an authorized split-shipment decision is recorded.
The difficulty with multi product print on demand orders is not simply that one checkout contains several SKUs. The real problem is that those lines can require different artwork, blanks, substrates, machines, finishing steps, operators, packaging, or production locations. One customer order can become several disconnected jobs unless the workflow deliberately reconnects them before shipment.
The operating principle is straightforward: optimize production around compatible work, but control fulfillment around the complete customer order. This lets a shop reduce changeovers without allowing a finished shirt, sticker sheet, sign, card pack, or insert to lose its relationship to the order that created it.
Define complexity by routing, not SKU count
A five-line order is not automatically more difficult than a two-line order. Five sticker variants using the same substrate, print mode, laminate, cut process, and package may travel together. A two-line order containing a personalized garment and a rigid sign may cross separate production cells, material stores, quality checks, and packing methods.
Classify an order by the operational differences among its lines. The classification should happen before work is released, not after the first line reaches packing.
| Complexity factor | Lower-complexity condition | Higher-complexity condition |
|---|---|---|
| Production route | Lines use the same work centers | Lines split across different machines, cells, or facilities |
| Materials | Common substrate, blank, or consumables | Several material families or uncertain availability |
| Artwork | Approved static files | Personalization, variable data, or unresolved versions |
| Finishing | Common finishing sequence | Different curing, trimming, laminating, pressing, or assembly |
| Packing | Products fit one approved pack method | Incompatible dimensions, protection needs, or inserts |
| Exceptions | All lines ready and routine | Substitution, quality hold, deadline, or split-shipment risk |
Use these factors to assign a handling class such as standard, coordinated, or exception-managed. The labels matter less than the response attached to them. A coordinated order might require material reservation and a consolidation location, while an exception-managed order might require supervisor review before production release.
When catalog planning includes additional print product options, operations should approve the production route, material rules, quality criteria, and packing method for each new product before it becomes an active SKU.
Make the customer order the control unit
The parent order record should answer one question at any time: what must still happen before this order can ship? Each line then needs its own work packet so it can travel through the appropriate route without losing its parent relationship.
A practical production record should include:
- Parent order ID and unique line ID
- SKU, variant, quantity, and personalization data
- Approved artwork version or immutable file reference
- Required blank, substrate, ink, laminate, transfer, insert, and packaging components
- Production route and required work centers
- Promised ship date, internal due time, and service level
- Line status, quality status, and consolidation location
- Packing instructions and required inserts
- Shipment status, including hold, authorized partial shipment, or complete
- Exception code, owner, next action, and deadline
Structured records do not require an enterprise platform. A small shop can begin with controlled shop tickets and a shared order register. The critical requirement is that identifiers and statuses use consistent definitions. Free-text notes should supplement the record, not replace routing, quantity, version, and completion fields.
For shops progressing toward system integration, CIP4’s JDF and XJDF overview provides a useful model for exchanging order, production, finishing, and delivery information across print workflows. JDF or XJDF adoption is not mandatory, but the underlying lesson applies at any scale: production data should move with the job instead of being reconstructed at every handoff. Shops receiving orders from multiple channels should also normalize incoming data before release, as described in this marketplace-to-production workflow.
Map demand and capacity by work center
Printer capacity alone does not determine whether a multi-product order ships on time. Preflight, picking, curing, trimming, heat pressing, assembly, quality control, consolidation, packing, or carrier closeout can become the constraint.
Track demand in units that expose the actual workload: orders arriving by hour, lines per order, units per line, product-family mix, standard work minutes by route, queue age, due time, and the share of orders requiring consolidation. Then compare required work minutes with available staffed minutes at each work center.
For example, suppose a hypothetical daily release requires 300 trimming minutes, 420 pressing minutes, and 240 packing minutes. If each cell has 360 staffed minutes available, pressing is already overloaded even if the printers have spare capacity. Adding print volume will increase work in process without improving completed-order throughput. The useful response is to rebalance labor, adjust the release window, reduce setup time, or change the promised service level—not merely run the printer faster.
Maintain an aging view as well as a workload view. A small line waiting for its companion products can threaten an order even when its own production cell appears lightly loaded. The complete order’s due time should influence line priority.
Reserve materials before releasing work
A production-ready line should have more than approved artwork. Its required blank or substrate, consumables, finishing components, inserts, and packaging should either be allocated or covered by a defined replenishment rule. Otherwise, the shop can complete several lines and discover that one unavailable component prevents shipment.
Reservation does not always mean physically moving every item into a kit. It means preventing the same available stock from being promised to several released jobs. High-risk, personalized, or scarce components may justify physical staging. Common consumables may be controlled through available-to-promise quantities and replenishment triggers.
Define substitutions before shortages occur. The record should state whether a blank, substrate, finish, package, or insert can be replaced, who can approve the change, and whether new artwork or customer authorization is required. An operator should not have to improvise this decision at the machine.
Batch production without breaking order integrity
Producing every order from beginning to end can simplify control, but it often creates frequent material and equipment changes. Batching everything into large product-family runs can improve machine efficiency while increasing queue time and making consolidation harder. Most operations need a controlled middle ground.
- Confirm that artwork, materials, routing, and due-date data are complete before release.
- Group lines with compatible production requirements, such as substrate, blank type, print mode, color setup, or finishing route.
- Keep the parent order ID and line ID on every digital queue entry, traveler, bin, or label.
- Set a defined batching window so work does not wait indefinitely for a larger group.
- Confirm quantity and quality at the end of each route, then mark the individual line complete.
- Move completed lines to an order-specific consolidation location or scan them into a controlled holding state.
- Escalate aging lines and orders whose remaining work threatens the promised ship time.
A wave model releases a planned group at set times. Continuous or waveless release feeds work as capacity becomes available. Exception batching pulls urgent, remake, or material-constrained work into a separate controlled queue. None is universally best. The right model depends on arrival patterns, setup costs, route variability, staffing, and service levels.
The guardrail is the same under every model: a production batch may contain lines from many orders, but completing the batch does not mean those customer orders are ready to ship.
Use positive reconciliation at consolidation and packout
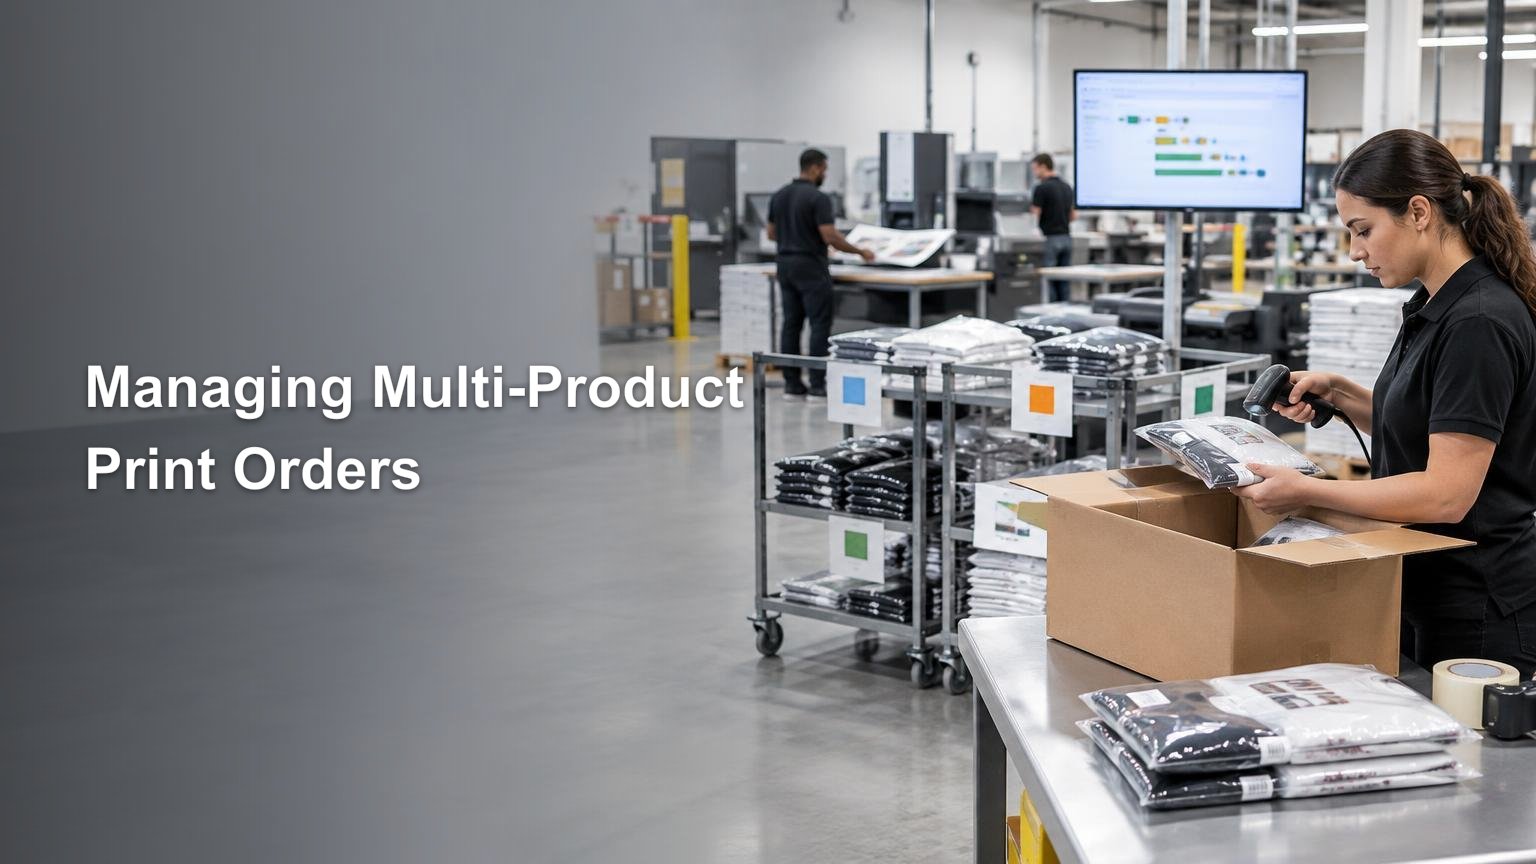
Consolidation is a controlled production stage, not a shelf where completed items accumulate. Each line should enter with an identity, verified quantity, quality status, and location. The order becomes pack-ready only when the system positively confirms every required line and component.
A pack checklist should be generated from the order record rather than operator memory. It should cover products, quantities, variants, personalization, inserts, protective materials, package type, and any shipment-specific instruction. Barcode-assisted confirmation can reduce manual matching effort when volume and product variety justify it.
The GS1 barcode standards overview describes identification systems that connect products, logistics units, locations, and traceability events. A shop does not need to implement the full GS1 system to apply the principle: use unique, machine-readable identifiers to preserve identity across production and fulfillment handoffs.
A basic scan-to-pack sequence is: scan the order, scan each expected line, reject unexpected or duplicate scans, confirm required inserts, validate the package, and create the shipping label only after reconciliation. Manual operations can mimic the same control with numbered bins and signed checklists, provided completion requires an explicit match rather than an assumption.
Protect label generation from premature release. A printed carrier label can create the false appearance that an order is finished. Connect label creation or manifest closeout to pack completion, and use the broader paid-order-to-tracking workflow to define the surrounding handoffs.
Define split-shipment rules in advance
When one line is delayed, the shop needs a recorded decision: hold the complete order, split the available products, or escalate for review. Split shipments should not happen simply because some items are already near the packing station.
The policy should define who may authorize a split, which service levels permit it, who owns customer communication, how extra shipping cost is handled, and how the remaining lines stay visible. The first shipment record must identify what it contains, while the parent order remains open until all lines are shipped, canceled, or otherwise resolved.
Shipping rules also need jurisdiction-specific verification. For U.S. postal shipments, use the current Domestic Mail Manual available through the USPS publications resources when implementing mailability and package rules. Do not hard-code carrier assumptions from an old ticket, rate table, or remembered threshold.
Treat remakes as linked exception work
A remake should never appear as an unrelated new job. Create a remake ticket linked to the original parent order and line, preserving the SKU, artwork version, quantity, defect category, production route, shipment status, and the point where the defect was detected.
The remake workflow should also answer whether completed companion lines remain on hold, have already shipped, or require a second shipment. Quarantine suspect goods so they cannot re-enter consolidation, and assign the remake a priority based on the customer commitment and current order state rather than sending every remake blindly to the front of every queue.
Use consistent defect categories such as artwork mismatch, wrong material, print defect, finishing defect, quantity shortage, picking error, packing damage, or carrier damage when supported by evidence. Reporting by SKU, route, material, work center, and detection point can then reveal where prevention will have the greatest operational value.
Measure complete orders, not just machine output
A press can look productive while orders wait for one missing line. The operating dashboard therefore needs both work-center and order-level measures:
- Queue age and due-date risk by work center
- Time from order release to all-lines-complete status
- On-time shipment rate against the defined promise
- First-pass yield and remake rate by route and product family
- Pack accuracy and shipment-exception count
- Orders waiting at consolidation and the reason for each wait
- Material shortage incidents after job release
- Authorized partial shipments and unresolved remaining lines
Avoid adopting generic targets without understanding the product mix. Establish a clean baseline, segment the measures by route or order class, and improve the most common delay or error source. Averages alone can hide a small group of highly complex orders that consumes disproportionate coordination time.
Build the system in stages
Start with a disciplined order register, consistent shop tickets, explicit statuses, and controlled consolidation locations. Add barcode labels when manual identification becomes slow or error-prone. Integrate the order management, production, inventory, and shipping systems when duplicate data entry or delayed updates become the next constraint.
Software maturity is not the same as process maturity. An integrated platform cannot compensate for undefined status meanings, uncontrolled substitutions, missing artwork versions, or unclear split-shipment authority. Stabilize those rules first, then automate them. The same principle applies to artwork: establish the version and file handoff controls described in this print-on-demand artwork organization guide before expecting automation to route files safely.
The practical next step
Choose one recent multi-product order and map every handoff from checkout to carrier acceptance. Mark where its lines separated, how identity was preserved, when materials were reserved, where completion was recorded, and who authorized any exception. Any point that depends on memory, an unstructured message, or searching the shop floor is a control gap.
Efficient batching and accurate fulfillment can coexist. Organize production around compatible requirements, maintain line-level identity through every route, and keep the customer order as the final release unit. That combination improves throughput without sacrificing the order-level accountability needed to pack, ship, and remake multi-product work reliably.